Find noisy or rough gears on your production line. Compare MRLing gear roll testers for single flank, double flank and cluster gear measurement.
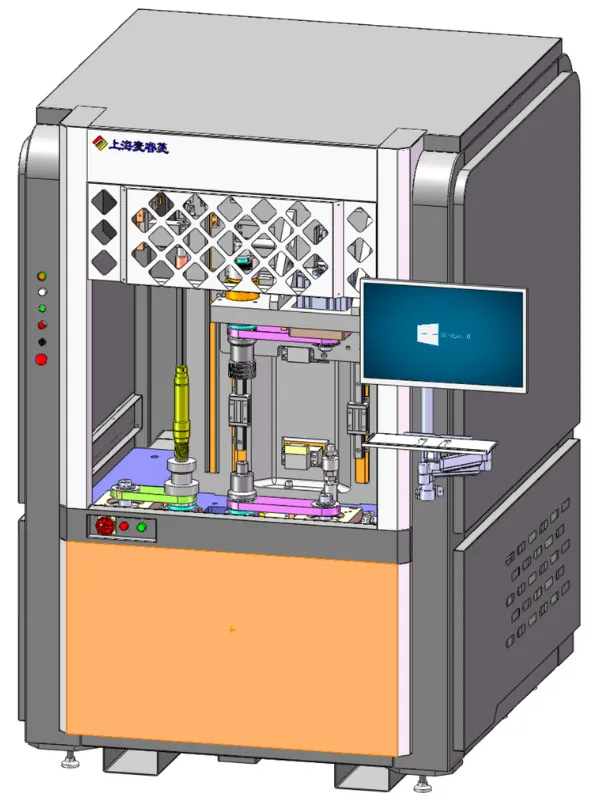
Measures transmission error, torsional vibration and tri-axial acceleration. Up to 60 s per part.
Learn More →
Fully automated in-line gauging of center distance variation. Robot loading. Spur and helical gears.
Learn More →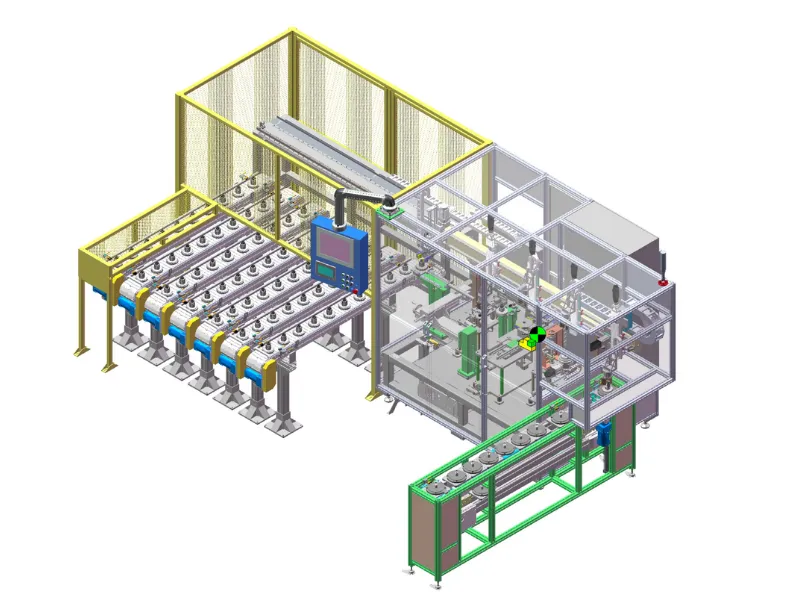
Six-station cell for cluster and stepped gears: true position, sorting, marking and barcode.
Learn More →Gear testers find gears that run rough or noisy before they reach the gearbox. Single flank testing shows how smoothly a gear runs. Double flank testing quickly checks runout and tooth-to-tooth variation. Use this table to compare our three machines.
| Machine | Test method | What it measures | Typical parts | Loading and cycle |
|---|---|---|---|---|
| Gear Single Flank Tester (MRL-M21) | Single flank rolling with a master gear | TE, TA and TX | Internal ring gears, input shafts, intermediate shafts, sun gears, final drive gears, motor shafts, stepped pinions | Manual loading, robot loading optional. Up to 60 s per part, without loading |
| Gear Double Flank Tester | Double flank rolling with a master gear | Center distance variation | Disc gears, shaft gears, differential cases with reducer gear, internal ring gears. Spur and helical | Robot loading and unloading. Fully automated in-line |
| Dual Gear Measurement | Double flank meshing of both gear steps | True position and precision classification, with laser marking, 2D barcode and sorting | Cluster and stepped gears. Spur and helical | Fully automated six-station cell, from loading to sorting |
TE means transmission error. TA means torsional vibration. TX means tri-axial acceleration. Specifications are for reference. Send us your gear drawing and we will confirm the details.
Start with the problem you want to find.
Use the MRL-M21 single flank tester to measure transmission error, torsional vibration and tri-axial acceleration. These readings help you find gears that can cause whine and noise.
See the MRL-M21The double flank tester loads parts by robot and measures center distance variation in a fully automated cycle. Modular fixtures help you change between gear types.
See the double flank testerThe dual gear measurement cell measures true position, sorts parts by precision grade, and adds laser marking and 2D barcode reading in one line.
See the dual gear cellAdd the optional double flank testing module to the MRL-M21, so one machine can do both tests.
See the optionsA gear tester, also called a gear roll tester, meshes a gear with a master gear and rolls them together. The machine measures how the gear runs, so you can find bad gears before they are assembled into a gearbox.
In single flank testing, one tooth side touches the master gear and the pair rolls together. The machine measures transmission error and vibration, which relate to how the gear sounds in use. In double flank testing, both tooth sides touch the master gear, and the machine measures how the center distance changes as the gears roll. It is a fast check of runout and tooth-to-tooth variation.
Single flank testing is the better choice, because it reads transmission error, torsional vibration and tri-axial acceleration. Double flank testing is faster and is a good fit for in-line checks of runout. You can also have both: the MRL-M21 has an optional double flank testing module.
The MRL-M21 covers internal ring gears, single external gears (input shaft, intermediate shaft, sun gear, final drive gear, motor shaft) and dual external gears such as stepped planetary pinions and cluster gears. The double flank tester covers disc gears, shaft gears, differential cases with reducer gear and internal ring gears. The dual gear measurement cell is made for cluster and stepped gears. We support both spur and helical gears.
The double flank tester and the dual gear measurement cell are fully automated. The double flank tester uses robot loading and unloading. The MRL-M21 is loaded by hand and can be expanded to robot loading.
The MRL-M21 takes up to 60 seconds per part for TE and TA, not including loading and unloading. For the other machines, the cycle time depends on your gear. Send us your drawing and we will confirm the time.
Yes. The double flank tester and the dual gear measurement cell use modular fixtures for fast model changeover, and the dual gear cell also has quick-change tooling. On the MRL-M21, you choose the meshing method for your gear: single external, dual external or internal ring gear.
We also build inline inspection machines for brake discs and shafts. See all machines on the products page.
Send us your gear drawing and your test needs. Our engineers will recommend the right machine.
Request a Quote